
Company News
Truck-mounted unit improves water use
The Amanzi Recycling Combination Vac Jet is capable of handling various maintenance tasks, including wet suction, high-pressure jetting, debris removal and continuous water recycling
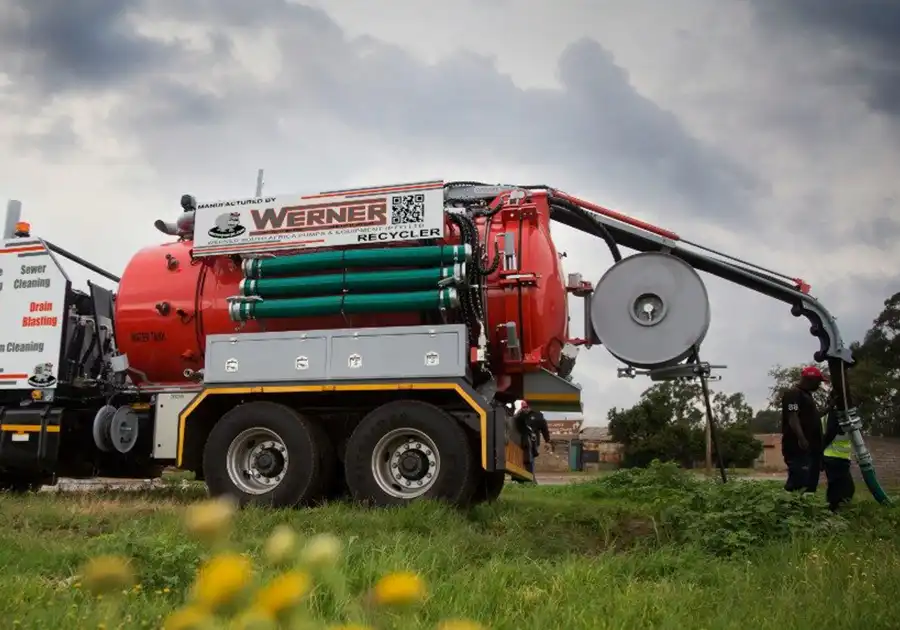
Aligned with the requirements of remote mining environments, where access to clean water is limited, high-pressure jetting and vacuum equipment manufacturer Werner Pumps has developed a truck-mounted recycling unit that simplifies maintenance tasks and improves water use.
Engineered for South African conditions, Werner Pumps national sales manager George Jolly says the Amanzi Recycling Combination Vac Jet unit consolidates several functions into one system capable of handling various maintenance tasks, including wet suction, high-pressure jetting, debris removal and continuous water recycling.
The unit draws water directly from a drain system, filters and reuses it, consequently enabling not only the teams to continue working without making return trips to refill tanks but also the truck to operate with water available on-site, even if dirty or contaminated.
In instances where no water source is available, the truck can be filled once and will vacuum and jet simultaneously, continuously reusing the same water it started with, says Jolly.
Using on-site water and reducing refilling cycles enable mines to reduce operational disruptions and costs. The unit also separates solids from liquids, re-jetting the vacuumed water to maintain drainage systems throughout a mine.
Cleaning drain systems more quickly and efficiently enables the system to deliver time efficiencies and cost savings, in addition to conserving a significant volume of potable water, compared with conventional high-pressure jetting systems that rely on large quantities of clean water, he adds.
“Without the recycling capability, trucks need to drive long distances to retrieve clean water. This costs money [for] fuel and maintenance, which pushes up your operational costs,” says Jolly, explaining that the unit can save up to 168,000 L of clean water during a jetting operation.
He highlights that integrating water-recycling pump units into a mine’s water stewardship strategy offers a practical means of embedding sustainable, water-wise practices into everyday operations.
Specifications and Configurations The Amanzi Recycling Combination Vac Jet comprises a 12,500 L 304-grade stainless steel tank and a 360° continuous slewing boom with a six-inch suction line.
It also features a single-cylinder pressure transformer jetting pump that can provide flow rates of up to 350 L/min at 205 bar, making it well suited to large-scale drain management, says Jolly.
The pump unit operates a hydraulically driven liquid ring vacuum pump at 3,100 m³/h, with an operational capacity of 3,000 m³/h, delivering effective industrial vacuuming of sludges and slurries typical of mine drainage environments, while the recycling jetting pump is engineered to handle small particles.
The truck-mounted vacuum and jetting unit also features a quiet, contact-free rotor vacuum pump alongside wireless remote control and real-time electronic monitoring. The wireless remote enables the rig’s operator to have a 360° view of the truck during operation, enhancing on-site safety and operation.
As the Amanzi unit is locally manufactured, Werner can offer shorter lead times on parts, which, in turn, reduces equipment downtime as opposed to imported alternatives, which can be subject to lengthy procurement delays.
The vacuuming and jetting platform can be fitted across a wide range of truck chassis options, enabling customers to align purchases with their preferred vehicle brands and existing fleets.
More specifically, Werner Pumps holds accredited truck-body builder status with various automotive manufacturers, including UD, Hino, Scania, Isuzu and MAN, and can build on most other chassis brands.
The 12,500 L configuration runs on a 6×4 chassis, while units of 15,000 L and larger are mounted on an 8×4 chassis. A 6×6 chassis option is also available for off-road conditions.
Werner Pumps also offers after-sales support, including repairs and maintenance, as well as a comprehensive range of accessories and spares such as high-pressure guns, lances, hoses and a tank-cleaning nozzle.
Werner Pumps’ flexible maintenance plans are available on one-, three- and five-year terms, with on-site maintenance support to decrease equipment downtime.
These offerings enable mining operations to configure the truck for their specific maintenance requirements and mitigates long lead times for parts, says Jolly, concluding that Werner Pumps works closely with customers to understand the challenges they face and recommend configurations that will support long-term reliability.
Related equipment
Equipment connected to this work.
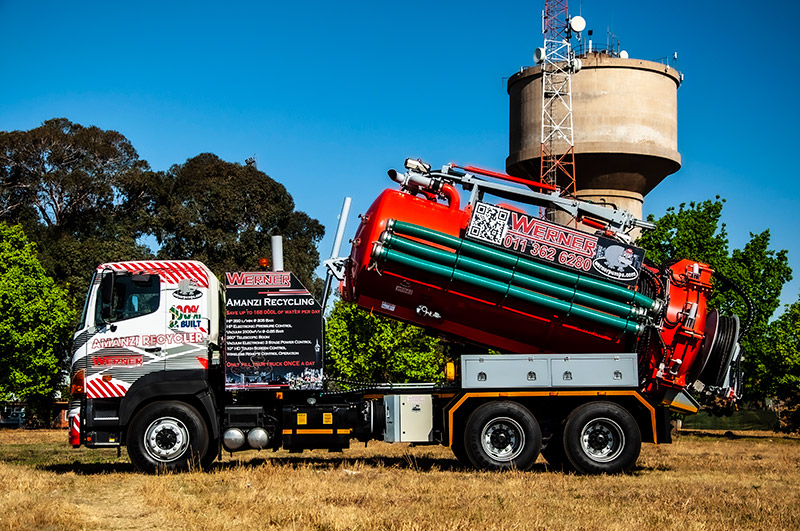
Amanzi Recycling Combination Units
The Amanzi Recycler combines forceful jetting, high-volume suction and continuous water recovery in one intelligent combination unit. Its oscillating filtration drum separates recovered water for immediate reuse, reducing refill journeys while cleaning continues. Designed and built in South Africa for harsh operating conditions and scarce resources, the Amanzi's robust stainless-steel construction, precise controls and serviceable layout translate into lasting capability in any demanding market.
View equipmentRelevant applications
Explore the complete working solution.
Water Recycling
Reuse recovered water during sewer and stormwater cleaning to reduce fresh-water demand and interruptions for refilling.